4.3.1 Cleaning
4.3.1 Cleaning
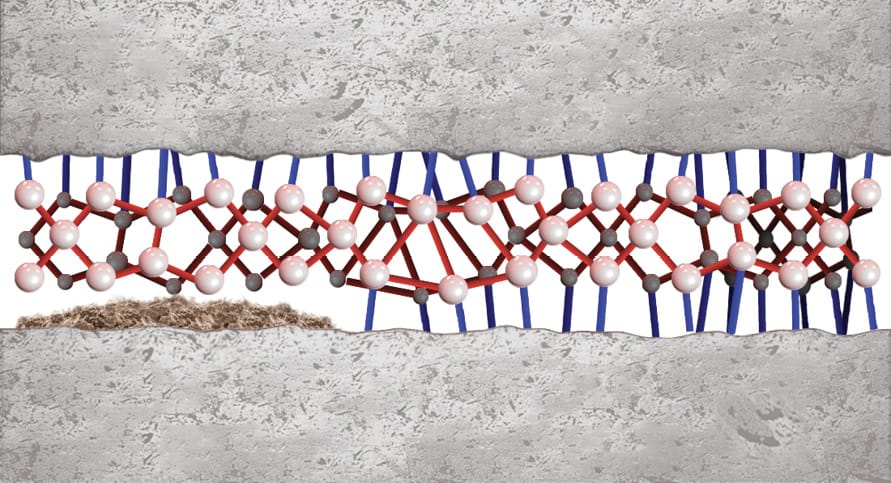
Any barriers to surface contact will reduce an adhesive’s bond strength. Such barriers include accidental contaminants like dirt, rust and oil or intentionally applied materials like detergents or protective films. Metal may be contaminated with cutting oil or corrosion inhibitors. Injection-moulded plastics typically have mould release on their surfaces. Table 9 shows some common sources of contamination.
| Source of Contamination | Contamination |
| Manufacturing processes | Release agents, graphite content in cast iron, drawing lubricants |
| Handling | Oils |
| Environment | Moisture, dirt and dust |
| Machining processes | Cutting fluids, swarf, corrosion inhibitors |
| Inactive layers | Oxide layers (metals) protective oil, e.g. black oxide steel bolts |
| Residues from galvanic processes | Metallic protective coatings like zinc, nickle, phosphate or chromate |
| Cleaning processes | Residues from alkaline baths or industrial cleaners, corrosion inhibitors |
One cleaning step to remove all contaminants is preferable. However, depending on the nature of the contamination on a substrate, multiple methods may be required. Multiple forms of contamination are typically present, especially on used parts. In addition to removing contaminants, the cleaner used must be compatible with the substrate and the adhesive. Cleaners must also follow health, safety and environmental standards, such as those for volatile organic compounds (VOC) and biodegradability. The drying time of a cleaner and the required equipment must also be considered in the choice of cleaners. Table 10 outlines considerations when choosing a cleaning process.
GET FREE ACCESS
TO THE DIGITAL MANUAL
Advance Your Technical Proficiency - Dive into Expert Knowledge
in Industrial Bonding.
Already have an account? Sign in here.